

Technical Proposal for ZT‑5050T Carbon Fiber Automatic Multi‑Stage Press
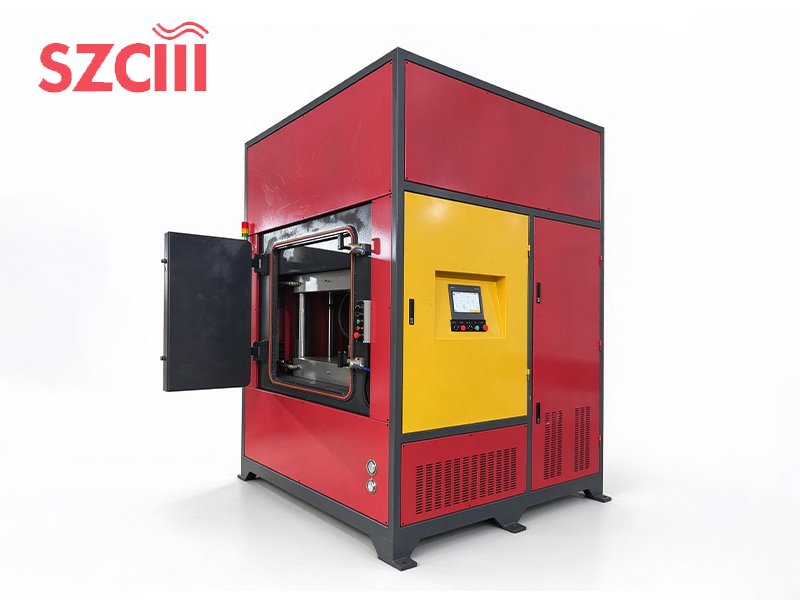
This proposal is designed for compression molding processes of carbon fiber and composite components. It adopts a five‑station serial layout of four hot‑press stations plus one cold‑press station, paired with an automatic mold transfer system and centralized electric control system. It realizes integrated continuous operations including heating, pressurization, heat‑holding & pressure‑holding, curing and cooling‑setting.
The equipment supports fully‑automatic whole‑line linked operation as well as independent operation of any single unit, meeting both mass‑production and small‑batch trial‑production requirements.
This solution addresses three core process pain points:
- Continuous execution of multi‑stage temperature/pressure curves cannot be completed within one single unit in traditional workflows, which requires manual mold transfer and causes sharp temperature drop of parts during transfer.
- Part deformation and internal stress induced by hot demolding.
- Batch stability risks caused by inconsistent process parameters across separate equipment.
Closed‑loop control of above‑mentioned issues is achieved within production cycle through serial hot‑press to cold‑press workflow and unified recipe management.
| Component | Qty | Function Description |
|---|---|---|
| Hot‑press Main Unit (Hot Station 1‑4) | 4 sets | Perform temperature rise, multi‑stage pressurization, heat‑holding & pressure‑holding curing. Each unit allows independent setting of process curves. |
| Cold‑press Main Unit (Cold Station) | 1 set | Receive parts after hot pressing, perform rapid cooling‑setting under pressure holding to suppress deformation and internal stress. |
| Automatic Mold Transfer System | 1 set | Servo‑driven; automatically transfers molds between hot stations and cold station according to production cycle; positioning accuracy satisfies mold‑closing requirements. |
| Heating & Temperature Control System | 1 set | Electric heating, zone‑divided temperature control, PID closed‑loop; programmable multi‑segment heating / heat‑holding curves. |
| Hydraulic System | 1 set | Provide 50‑ton clamping force; support multi‑stage pressure setting and pressure‑holding compensation. |
| Pneumatic System | 1 set | Multi‑stage pneumatic control for vacuum bag assistance, air‑bag pressurization and pneumatic actuators. |
| Cooling System | 1 set | Circulating cooling for cold station; equipped with chiller or factory cooling‑water interface. |
| Electric Control System | 1 set | PLC + touch screen; recipe management, multi‑unit linkage, fault alarm and safety interlock. |
| Item | Parameter | Remarks |
|---|---|---|
| Platen Size | 500 mm × 500 mm | Identical for hot stations and cold station |
| Daylight / Opening Height | 400 mm | Adjustable according to mold height |
| Nominal Pressing Force | 50 tons per unit | 4 hot‑press units + 1 cold‑press unit |
| Number of Stations | 4 hot stations + 1 cold station | Serial layout |
| Total Power | 70 kW | Including heating, hydraulic, servo and control power consumption |
| Power Supply | 380V / 3‑Phase / 50Hz | 60Hz‑compatible version optional |
| Overall Machine Dimension | Approx. 5000 mm (L) × 2444 mm (H) | Width subject to final drawing |
| Control Mode | PLC + Touch Screen, recipe‑based | Linked mode / single‑unit mode available |
| Temperature Control | Multi‑segment programmable, PID closed‑loop | Temperature accuracy and max. temperature subject to configuration |
| Pressure Control | Multi‑segment programmable | With pressure‑holding compensation |
| Pneumatic Control | Multi‑segment programmable | Equipped with precision pressure regulator and pressure detection |
Note: Maximum temperature limit, temperature‑control accuracy, heating / cooling rate, mold‑transfer cycle and other indicators shall be confirmed against final configuration and mold conditions, and can be specified item‑by‑item in the technical agreement.
Table 4‑1 Standard Molding Cycle (adjustable via process recipe)
| Step | Procedure | Actions & Process Key Points |
|---|---|---|
| 1 | Material Preparation & Mold Loading | Prepreg lay‑up, mold closing; mold fed through mold‑in port. |
| 2 | Mold Feeding & Mold Closing | Mold transfer mechanism delivers mold to Hot Station 1; low‑pressure mold closing and vacuum pumping (if required by process). |
| 3 | Temperature & Pressure Rise | Execute first‑stage heating and pressurization per recipe; resin flows and impregnates fibers. |
| 4 | Multi‑segment Heat‑holding & Pressure‑holding | Transfer mold between Hot Station 1‑4 by production cycle; complete progressive heating, constant temperature and pressure compensation to achieve step‑wise curing. |
| 5 | Hot‑state Mold Transfer | Automatically transfer mold to cold station under pressure‑holding status to avoid part spring‑back caused by mold opening. |
| 6 | Cooling & Setting | Cold station maintains continuous pressure‑holding; circulate‑cool down to demolding temperature; control cooling rate to reduce internal stress. |
| 7 | Mold Opening & Part Unloading | Open mold; finished part is taken out from mold‑out port for next production cycle. |
The whole line runs cyclically: after the first workpiece enters Hot Station 1, subsequent workpieces follow sequentially. Each station stays at different phases of “heating — curing — cooling” to realize continuous output. Under single‑unit mode, linkage function can be disabled. Each unit can run with independent recipes for sampling or small‑batch trial‑production.
5.1 Multi‑Stage Temperature Control
Each hot station is equipped with independent temperature‑control loops, supporting programming of no less than 8 segments of heating‑constant‑temperature‑cooling curves. Target temperature, heating rate and holding duration can be set for each segment. The system collects multi‑point platen temperature in real‑time with PID closed‑loop heating output regulation. Alarms and protective actions will be triggered for over‑temperature, abnormal heating rate, thermocouple disconnection and other fault conditions.
5.2 Multi‑Stage Pressure Control
The hydraulic system sets clamping pressure and pressurization rate segment‑by‑segment according to recipes, supporting stepped pressurization: low‑pressure pre‑pressing → medium‑pressure impregnation → high‑pressure curing. Pressure‑holding compensation is available during holding phase to offset pressure decay caused by resin flow and thermal expansion, ensuring consistent part compactness.
5.3 Multi‑Stage Pneumatic Control
The pneumatic circuit is fitted with precision pressure regulators and pressure sensors. Pneumatic setpoints can be configured segment‑by‑segment for vacuum‑bag assisted compaction, uniform air‑bag pressurization and sequential actions of pneumatic actuators. Pressure curves are time‑axis synchronized with temperature curves.
5.4 Recipe Management & Data Traceability
Built‑in recipe library on touch screen supports saving, recalling and copying product‑specific process recipes (temperature, pressure, pneumatic value, time, mold‑transfer cycle). Hierarchical permission management is available (Operator / Process Engineer / Administrator). Actual segment‑by‑segment production curves and alarm events are auto‑recorded during production and exportable by batch for quality traceability and process review.
The mold transfer mechanism adopts servo‑driven acceleration‑deceleration positioning control to transport molds among five stations along guide rails. Dual confirmation by mechanical limit and position detection ensures mold accurate alignment before mold‑closing is permitted, preventing platen & mold damage from eccentric load.
Mold‑transfer actions are interlocked with pressure and temperature status of each station: mold‑transfer commands will not be executed if any station is under unsafe conditions.
Three operation modes are supported:
‑ Full‑automatic linkage: auto mold transfer by production cycle
‑ Semi‑automatic: step‑by‑step manual confirmation
‑ Manual: inching mode for commissioning and troubleshooting
The cold station is embedded with circulating cooling loops, fitted with plate heat exchanger plus flow & temperature monitoring. Cooling‑medium temperature and flow rate are adjustable for controllable cooling‑rate.
Cooling water can be supplied by factory utilities or optional standalone chiller unit to eliminate dependency on unstable factory water temperature.
Designated pressure is maintained throughout cold‑station cooling. Parts shrink under constrained conditions to effectively mitigate warpage and dimensional deviation.
| Item | Description |
|---|---|
| Controller | Industrial PLC + color touch‑screen HMI; Chinese / English switchable interface |
| Linkage Control | Unified scheduling for five stations with configurable cycle time; alternatively switchable to five independent presses |
| Safety Protection | Emergency‑stop buttons, safety‑door / light‑curtain interlock, hydraulic over‑pressure protection, over‑temperature protection, anti‑intrusion protection for mold‑transfer zone |
| Fault Diagnosis | Alarm‑code indication, historical alarm log, trend curves of key parameters |
| Data Interface | Reserved Ethernet port; expandable for MES / upper‑computer data acquisition (optional) |
| Item | Requirement | Remarks |
|---|---|---|
| Power Supply | 380V / 3‑Phase / 50Hz, 70 kW | Dedicated power circuit recommended with 15% capacity margin |
| Compressed Air | 0.6‑0.8 MPa, dry & clean | Flow rate subject to pneumatic component configuration |
| Cooling Water | ≤30 ℃; flow & pressure as specified | Stand‑alone chiller optional |
| Civil Foundation | Flat concrete floor with sufficient load‑bearing capacity; reserved space for operation & maintenance around equipment | — |
| Site Environment | Well‑ventilated; corrosive gas prohibited | Exhaust system recommended for curing volatile emissions |
| Item | Qty | Remarks |
|---|---|---|
| Hot‑press Main Unit (50 ton, 500×500 mm) | 4 sets | Including heating platens and thermal insulation layers |
| Automatic Mold Transfer System | 1 set | Servo‑driven transfer mechanism |
| Pneumatic System | 1 set | Including precision pressure regulators |
| Cooling System | 1 set | Heat exchanger and flow monitoring included |
| Electric Control System & Operation Console | 1 set | PLC + touch‑screen |
| Random Technical Documentation | 1 set | Drawings, operation manual, electrical schematics, certificate of conformity |
| Spare Parts & Special Tools | 1 set | Per attached list |
Items to be provided by Customer: molds, plant infrastructure (power distribution to equipment incoming terminal, compressed‑air source, cooling‑water interfaces), hoisting & positioning coordination, test‑molding raw materials.
- Installation & Positioning: We provide foundation drawing and hoisting scheme. We guide equipment positioning, leveling and anchor bolt fixing, and complete power, water and pneumatic piping connection.
- Commissioning: Complete stand‑alone functional tests (hydraulics, heating, pneumatic circuit, mold transfer, alarm functions), linked‑cycle commissioning and no‑load continuous running test. Afterwards, support customer for mold‑loaded pressure test and first‑article trial production, optimizing process curves.
On‑site operation and process‑commissioning training is delivered, covering startup‑shutdown workflow, recipe creation & recall, daily inspection & maintenance, and common alarm handling. Practical operation assessment is conducted post‑training to ensure operator competence.
| Option | Description |
|---|---|
| Stand‑alone Chiller Unit | Controllable cooling‑water temperature; reduce dependency on factory water system |
| Vacuum System | Vacuum pump, vacuum‑bag interface and vacuum‑level monitoring |
| Mold Oil Heating Circuit | Oil‑temperature‑controller heating for uniform temperature rise of thick‑wall molds |
| Data Acquisition & MES Interface | Process‑curve upload, batch traceability, remote monitoring |
| Safety Light Curtain & Safety Fence | Upgrade personnel‑protection level for mold‑transfer zone |
| 60 Hz / Alternative‑Voltage Version | Adapt to overseas power grid (e.g. 440V/60Hz, 220V/60Hz) |
| English‑language HMI & English Technical Documents | Recommended standard for export projects |
This document serves as technical proposal only. All parameters and configurations shall be subject to the final technical agreement and mutually‑confirmed drawings.
